Industrial pumping equipment plays an important role in transferring liquids, chemicals, and other fluids across different industries. From chemical processing and pharmaceutical production to water treatment and manufacturing, businesses require reliable pumps to maintain smooth daily operations. Choosing suitable pumping equipment helps improve productivity, reduce maintenance concerns, and support efficient fluid handling.
Different industrial applications require different types of pumps depending on liquid properties, pressure requirements, and operating conditions. This is why selecting experienced Diaphragm Pump Manufacturers is important for businesses looking for dependable pumping solutions.
Understanding Diaphragm Pumps and Their Industrial Applications
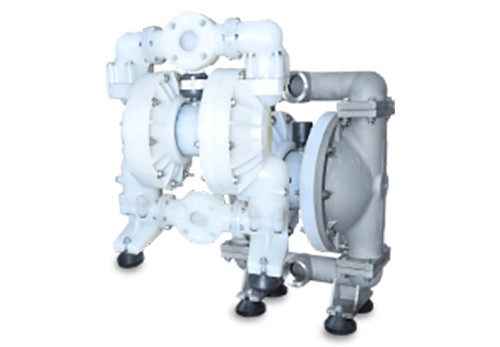
A diaphragm pump is a positive displacement pump that uses a flexible membrane to transfer liquids. The diaphragm moves back and forth, creating pressure differences that allow liquid to enter and leave the pumping chamber.
These pumps are widely used in chemical processing, pharmaceutical production, wastewater treatment, food processing, and manufacturing industries. Depending on their design and construction materials, they can handle various liquids, including certain corrosive, abrasive, and viscous fluids.
Professional Diaphragm Pump Manufacturers focus on developing pumping equipment that meets different industrial requirements while maintaining reliable fluid transfer.
Important Features of Diaphragm Pumps
Leak-Resistant Operation: Suitable diaphragm pump designs can reduce leakage risks because the pumping mechanism uses a flexible membrane to separate the liquid from other components.
Chemical Compatibility: Different diaphragm and pump body materials are available for handling various industrial chemicals.
Versatile Applications: These pumps are used for transferring chemicals, paints, wastewater, and other compatible industrial liquids.
Easy Maintenance: Regular inspection of diaphragms, valves, and connections helps maintain reliable pump performance.
Before purchasing a diaphragm pump, businesses should check liquid compatibility, required flow rate, operating pressure, and temperature limits. Reliable Diaphragm Pump Manufacturers can help buyers select suitable equipment according to their specific applications.
Why Choose Centrifugal Pump Manufacturers for Efficient Fluid Transfer?
Many industries require pumping equipment that can move large quantities of liquids continuously. Centrifugal pumps are commonly used for these applications because they operate through a rotating impeller that transfers energy to the liquid.
Experienced Centrifugal Pump Manufacturers develop pumping solutions for water supply, irrigation, industrial cooling, chemical processing, and general fluid circulation.
These pumps are suitable for applications where their hydraulic design matches the required flow rate and operating head. Their construction can vary depending on the liquid being handled and the working environment.
Key Benefits of Centrifugal Pumps
Continuous Liquid Movement: Centrifugal pumps are commonly used in processes that require steady fluid circulation.
Wide Applications: They are used in water treatment, manufacturing, agriculture, power plants, and industrial processing.
Different Designs: Various pump configurations are available to meet different pressure and flow requirements.
Operational Efficiency: Correct pump selection and installation can help improve energy use and overall system performance.
Before selecting a centrifugal pump, buyers should evaluate flow capacity, total head, impeller design, liquid properties, and motor requirements. Professional Centrifugal Pump Manufacturers can provide guidance on choosing suitable pumping equipment.
Understanding Mud Pump Manufacturers and Their Industrial Applications
Some industrial operations involve handling muddy water, drilling fluids, and liquids containing suspended solid particles. These applications require specialised pumping equipment designed according to the nature of the fluid and working conditions.
Reliable Mud Pump Manufacturers develop pumps for applications such as drilling operations, construction projects, mining, and industrial fluid transfer.
Mud pumps are designed to move fluids that may contain suspended solids. Their construction, internal components, and material selection depend on the type of mud, particle size, pressure requirements, and operating conditions.
Important Features of Mud Pumps
Heavy-Duty Construction: Suitable construction materials help pumps withstand demanding operating environments.
Handling Suspended Solids: Mud pumps are designed for specific slurry and drilling-fluid applications, depending on their configuration.
Industrial Applications: These pumps are used in drilling, mining, construction, and other specialised operations.
Application-Based Design: Different pump designs are available depending on fluid density, pressure, flow rate, and solid content.
When selecting a mud pump, businesses should consider fluid characteristics, particle concentration, required pressure, flow capacity, and maintenance requirements. Experienced Mud Pump Manufacturers can help identify suitable equipment for different industrial applications.
How to Choose the Right Industrial Pump Manufacturer
Selecting the right manufacturer is an important part of purchasing industrial pumping equipment. A dependable manufacturer understands different industry requirements and provides suitable products based on specific applications.
Here are some important factors to consider before making a purchase:
Product Quality: Check construction materials, manufacturing standards, and overall pump design.
Technical Specifications: Compare flow rate, pressure, temperature limits, and liquid compatibility.
Industry Experience: Consider the manufacturer’s experience in producing different industrial pumping solutions.
Product Range: Explore available pump models to identify suitable equipment for your application.
Technical Support: Choose a manufacturer that provides product guidance and maintenance assistance.
Comparing these factors helps businesses make informed decisions and select pumping equipment that supports long-term operational requirements.
Why Choose JEE Pumps Limited?
When searching for reliable industrial pumping equipment, businesses should consider manufacturers that understand different fluid-handling requirements. JEE Pumps Limited offers industrial pumping solutions for various applications across different industries.
Selecting suitable pumping equipment requires understanding the type of liquid, operating pressure, flow rate, temperature, and installation conditions. These factors help determine the most appropriate pump design for a particular process.
Whether an application involves chemical transfer, water circulation, or specialised industrial fluid handling, selecting the correct pumping solution is important for maintaining smooth operations.
JEE Pumps Limited is a manufacturer businesses can explore when looking for industrial pumping equipment. Buyers should review available product specifications and discuss their application requirements to identify suitable solutions.
Conclusion
Choosing the right industrial pump is essential for reliable fluid transfer and smooth business operations. Diaphragm pumps are useful for handling various industrial liquids, centrifugal pumps support continuous fluid movement, and mud pumps are designed for demanding applications involving drilling fluids and suspended solids. Businesses should compare product quality, material compatibility, technical specifications, and maintenance requirements before purchasing. JEE Pumps Limited is a manufacturer businesses can explore for industrial pumping solutions suited to their operational needs.